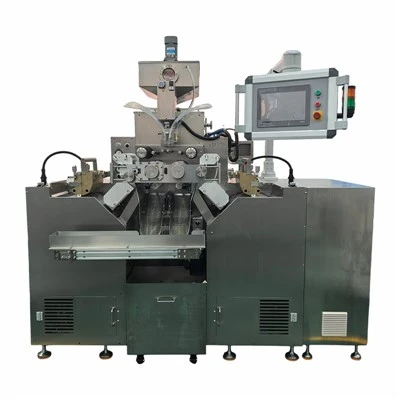
Hey everyone, it’s Jake from the bottle filling machine side, and today we’re diving into something that’s kept so many packaging teams up at night: leakage during the filling process. I’ve talked to 100+ facility managers and line operators over the years, and 8 out of 10 of them say a single leak mid-run can cost them thousands—wasted product, downtime to clean up, and even damaged packaging that cuts into their bottom line. The worst part? A lot of leaks aren’t from bad machines, they’re from small, easy-to-miss things that people either skip over or don’t realize matter. As someone who’s designed, serviced, and fixed these machines for years, I’m gonna break down exactly how to stop leaks cold—no jargon, just real stuff that works. Bottle Filling Machine
First off, let’s get one thing straight: I see a lot of people jump to blaming the machine right away when a leak happens, but 30% of the time it’s not the machine at all—it’s the pre-fill prep. I’ve had a client run a 20-hour fill line for months with the same machine, and then suddenly every 5th bottle was leaking. Turned out they were rushing the bottle inspection step and using the same old reusable cotton cloth to wipe the necks. Cotton leaves tiny lint fibers that get stuck between the bottle neck and the cap, right? Those fibers create a tiny gap that seals can’t cover, and before you know it, you have a slow leak that turns into a puddle on the line. The fix here? Ditch the cotton cloths. Use lint-free microfiber wipes, and make sure every bottle’s neck is dry before it even touches the capper. Also, don’t skip the visual check—no need for fancy cameras right away, just have an operator glance at every 10th bottle to make sure there’s no dust, leftover moisture, or even a tiny scratch on the neck glass or plastic. I can’t tell you how many times a scratched bottle neck is the culprit for a leak that people waste hours troubleshooting the machine for.
Next, let’s talk about the filling nozzle. This is the part that actually does the work, so it makes sense if it’s messed up, you get leaks. A lot of operators don’t clean the nozzle properly between runs—even between different products, if you’re switching from juice to soda, leftover syrup can gum up the nozzle tip, making it not seat right against the bottle. Wait, there’s also this: a lot of people crank the nozzle down super tight to “make sure it doesn’t move” during filling. No! If you clamp the nozzle too hard, it deforms the tip, or leaves a tiny indent on the bottle’s neck that will leak once the cap goes on. The sweet spot is where the nozzle sits flat against the bottle’s top, no give, no indent—if you press down gently and it rocks at all, you’re too loose; if you see a mark when you pull it up, you’re too tight. I also recommend checking the nozzle for wear every week, even if it looks fine. Most nozzles are made of stainless steel or food-grade plastic, and over time, the constant pressing and cleaning can wear down the edges. A worn nozzle edge won’t make a proper seal, so you get product seeping out while it’s filling, or air getting in that messes with the fill level and leads to leaks later. If you see any tiny nicks, dents, or just a dull edge on the nozzle, replace it—this is a $10 part that saves you hundreds in wasted product.
Then there’s the capper, and let’s be real, caps are where so many leaks happen. First, not all caps are made equal, but even the right cap will leak if the capper isn’t calibrated. A common mistake is setting the capper torque too high or too low. Too low, and the cap spins off a little, leaving a gap; too high, and you crack the bottle neck or strip the cap’s threading (and stripped caps can’t seal, obviously). How do you get the torque right? Don’t just go by the machine’s numbers—test with a sample cap, put it on a test bottle, and then use a cheap torque wrench (you can grab these at any hardware store for under $20) to check how much force it takes to turn the cap slightly. The sweet spot is usually 15-25 in-lbs for plastic bottles, a bit higher for glass, but it varies by cap size. Also, watch the capper head when it’s running. If you see the head bouncing or skipping during the spin, that means it’s not applying even pressure to the cap, so some caps will be loose and some too tight. If your machine has adjustable capper head rollers, make sure they’re aligned with the cap’s threading—too high, and they won’t grip; too low, and they’ll scrape the cap and mess up the seal. I’ve had clients who skipped this calibration and were getting a 5% leak rate, just because the capper roller was out of line by a millimeter.
Wait, I almost forgot about the fill level! This is a big one that people overlook, especially with carbonated drinks. If you overfill a bottle, the product has nowhere to go when you put the cap on—so it seeps out around the neck or under the cap, that’s a leak. For carbonated stuff like soda or sparkling water, you have to account for the foam, right? If you fill it to the very top right when the soda’s flat, once it carbonates and builds pressure, it expands and leaks out. How to fix this? Use a time-based fill machine with a pre-programmed delay for carbonated products, or a volumetric filler that adjusts for foam. A lot of cheap fillers just dump product in fast, which creates way more foam. Slow down the fill rate for carbonated goods—fill 80% first, wait 2 seconds for the foam to settle, then top off the rest. For non-carbonated, just set the fill level to leave a ¼ inch gap at the top of the bottle. That small gap might seem like nothing, but it prevents that pressure buildup that causes so many post-fill leaks. Also, check for pressure in the filling system itself. If your tank has too much internal pressure, it’ll push product out of the nozzle when it’s not even seated on a bottle. That’s called a “dribble fill,” and it leaves product on the outside of the bottle neck, which makes the cap not seal right. I once had a craft brewery client who was losing $500 a day in beer to dribble fills because their tank pressure was set 2 PSI too high—simple fix, no new parts needed.
Now, for the machine maintenance side—this is the stuff most people put off until something breaks, but it’s the secret to preventing leaks long-term. Let’s start with seals. Your bottle filling machine has dozens of O-rings and gaskets, right? They’re small, they get exposed to product, moisture, and cleaning chemicals, so they wear out fast. A worn O-ring on the nozzle, or the seal between the filling head and the tank, can cause constant leaks that you’ll never fix by adjusting other parts. The rule of thumb here is: replace all O-rings and gaskets every 3 months, no matter how good they look. Even if they don’t look cracked, they can lose their elasticity, so they don’t seal anymore. If you’re running acidic products like juice or soda, that wears seals even faster—maybe every 2 months. Also, when you replace seals, make sure you use food-grade ones, not the cheap generic ones you find at the auto parts store. I’ve seen generic O-rings swell or break after a week of being in contact with orange juice, leading to total machine failure. Stick to the ones your machine manufacturer recommends.
Another maintenance thing: alignment of the entire line. If the filling heads or the capper are even a tiny bit off, they won’t line up with the bottle correctly. A bottle that’s misaligned means the nozzle isn’t sitting flat, the capper isn’t gripping the cap right, and boom—leaks. How do you check alignment? Stop the line, put a test bottle on the conveyor, run the machine through a cycle, and see where the nozzle lands. If it’s off by more than a hair (like, a millimeter), adjust the conveyor guides or the filling head mount. I do this with every new client I work with, and it cuts their initial leak rate by 70% almost every time. Most machines have adjustable mounts for the heads, so it’s not a hard fix at all—just takes 10 minutes.
Wait, let’s talk about common mistakes people make when running the machine, too. A lot of operators push the machine to run faster than its rated speed, right? If your machine is rated for 50 bottles a minute, don’t try to cram 65 through it. Faster speed means the conveyor is moving bottles too fast, so they don’t line up perfectly with the filling heads, the nozzle can’t seat right, and the capper skips. That’s a surefire way to get leaks. Another thing: don’t reuse caps. I know, some facilities save leftover caps for the next run, but if a cap sits out for even a day, it can collect dust, get bent, or have tiny debris stuck on the threading. Use fresh, unopened caps for every run. I had a sauce company that saved caps for a week, and their leak rate went from 1% to 8%—they switched to fresh caps, and it dropped right back down.
Now, let’s get to the troubleshooting part, in case you’re already dealing with leaks. If you’re noticing leaks only at the start of a run, that’s almost always from leftover product in the nozzle or the fill head from the last run. Flush the lines with water for 30 seconds before starting, that clears out the gunk. If leaks happen only at the end of a run, that’s probably pressure buildup—turn down the tank pressure, or make sure the relief valve is working. If you have random leaks, not consistent, that’s usually worn seals or misaligned heads. If all caps are leaking, check the torque and the capper alignment, not the caps themselves.
Look, I get it—no one wants to deal with leaks. They’re messy, they cost money, they frustrate your team. The good news is, 90% of leaks are preventable with small, consistent steps, not expensive machine upgrades. As someone who sells and services bottle filling machines, I always tell my clients: don’t wait for a leak to fix something. Do the weekly checks, replace the small parts on schedule, don’t push the machine too hard, and spend 5 minutes prepping bottles instead of rushing.
If you’re dealing with a leak issue that you can’t figure out, or you’re looking for a new bottle filling machine that’s built to cut down on these exact problems, hit us up to chat. We can walk you through your current setup, troubleshoot what’s going wrong, or even help you design a line that fits your product and keeps leaks to a minimum. No sales pitch, just real advice from someone who’s been in this game for years.
Oh, and one last thing—when you do clean your machine, don’t use harsh chemicals that eat away at seals and nozzles. Stick to the food-grade cleaners recommended for your machine, and make sure you rinse everything well. Residue from chemicals can cause gunk buildup that leads to leaks too.
At the end of the day, leakage during filling isn’t a flaw in your process or your machine—it’s just a small detail that’s easy to get right. Take it from me, I’ve fixed lines that were losing $10k a week to leaks with $20 worth of parts and 10 minutes of calibration. That’s the stuff that moves the needle, not fancy tech. Now go check your nozzle, that’s probably where the first fix is.
Bottle Filling Machine References:
- Packaging Machinery Association. (2022). Best Practices for Bottling Line Leak Prevention. Industry Technical Bulletin.
- Food and Drug Administration. (2021). Food-Grade Components and Maintenance Guidelines for Packaging Equipment. FDA Compliance Guidance.
- Journal of Packaging Technology and Science. (2020). Factors Affecting Seal Integrity in Bottling Operations. Peer-Reviewed Research Paper.
- Global Bottling Solutions. (2023). Common Operational Mistakes Leading to Filling Line Leaks. Service Report for Beverage and CPG Facilities.
Wenzhou Vitol Machinery Co., Ltd.
As one of the most professional bottle filling machine manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy customized bottle filling machine made in China here from our factory. Also, quotation is available.
Address: #16 Yongen Road, Longwan Area, WenZhou, Zhejiang, China
E-mail: leapeng01@gmail.com
WebSite: https://www.vitolsoftgel.com/
